Coolant recycling,
engineered for
machine shops.
Coolant recycling, particulate filtration, tramp-oil separation, and sump-cleaning equipment for contract job shops, captive machining cells, screw-machine operations, and grinding facilities. These operations may use CNC, conventional, or mixed equipment.
- 40+ yrs
- fluid-management engineering experience
- up to85%
- reduction in new fluid purchases with C.R.O.S.S.
- 99.75%
- tramp oil & particulate removed by C.R.O.S.S., by volume
- 24/7/365
- clean coolant available with C.R.O.S.S.
Compare equipment by operating profile
Select the closest operating profile to review the typical fluid conditions, equipment roles, and system configuration.
Sump-side maintenance: T.O.S.S. + Green Machine
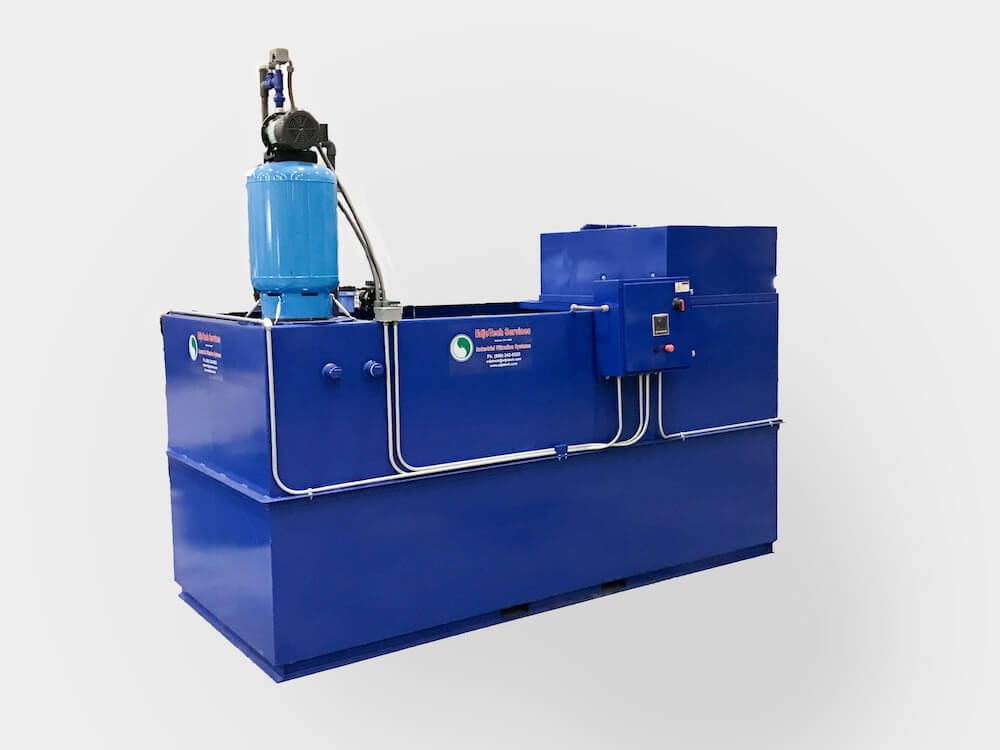
For machine shops that maintain individual reservoirs sump by sump, dedicated equipment provides reservoir-level coolant maintenance. T.O.S.S. controls tramp oil, while the Green Machine reduces sump-cleaning labor. C.R.O.S.S. can be evaluated when fluid consumption, disposal volume, or service workload creates a shop-wide recycling requirement.
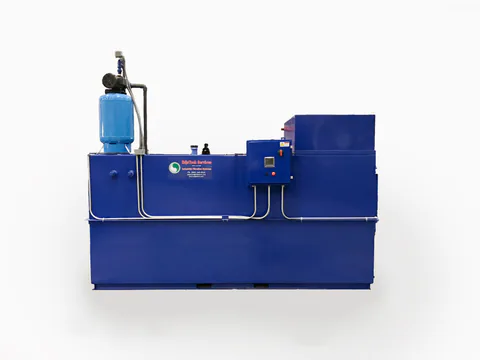
Coolant-management equipment built for machine shops
EdjeTech builds and services coolant-management equipment in Sullivan, Ohio. The company combines more than 40 years of fluid-management experience with product-specific performance and application support for system sizing, coolant compatibility, replacement parts, and ownership requirements.
| Number | Measure | Detail | Value |
|---|---|---|---|
| 01 | Engineering experience | More than 40 years building and servicing fluid-management equipment in Ohio. | 40+ yrs |
| 02 | C.R.O.S.S. fluid savings | Reduce new coolant purchases by up to 85% while removing 99.75% of tramp oil and particulate by volume. | Up to 85% |
| 03 | C.R.O.S.S. disposal savings | Reduce waste-disposal costs by up to 90%, depending on the application and operating conditions. | Up to 90% |
| 04 | Application engineering | Review coolant, contaminants, required flow, and facility layout before system selection. | 1 review |
Identify the operating problem
Coolant odor, surface oil, rising disposal cost, slow sump cleaning, and bacterial growth point to different equipment requirements.
- 01Persistent coolant odor or rapid degradationCoolant odor diagnostic →
- 02Tramp oil collecting on reservoir surfacesTramp-oil control guide →
- 03Increasing coolant disposal costsEstimate recycling savings →
- 04Excessive sump-cleaning labor and downtimeGreen Machine sump cleaning →
- 05Shop-wide coolant recycling requirementsC.R.O.S.S. specifications →
- 06Automated bacteria control without routine biocide additionBacteria and odor control →
What each system handles
Select equipment by coolant type, contaminant, required flow, reservoir size, and maintenance requirement.
| Equipment | Role | Application | More information |
|---|---|---|---|
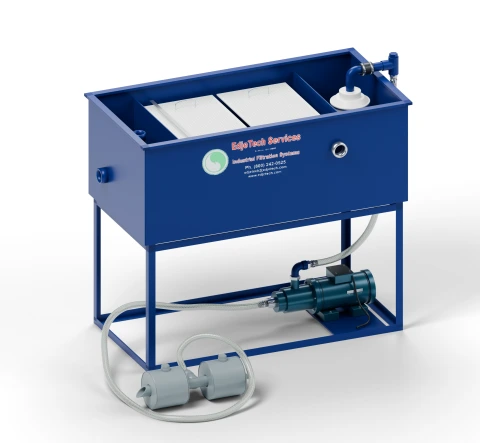
| C.R.O.S.S.2–25 GPM | Recycling | The central recycling system for machine shops with shop-wide coolant recovery requirements. Portable dirty-coolant collection is standard, with optional clean-coolant piping or a hybrid delivery configuration. | View → |
| Green Machine55–70 GPM | Sump cleaner | Air-powered portable sump vacuum. A typical manual cleanout that can require about four hours can be completed in approximately 15 minutes. The unit is the recommended EdjeTech equipment for portable batch transfer. | View → |
| T.O.S.S.2–50 GPM | Tramp oil | Autonomous tramp-oil separation for individual machine sumps, large reservoirs, pits, and parts washers. | View → |
| Paper bed + magneticModules | Filtration | Run alone or combined: a 98%-efficient ferrous separator paired with a paper bed for non-ferrous and general solids. Grinding and screw-machine chip loads. | View → |
| S.O.F.Oil-side | Straight oil | For shops on straight cutting oil, and for filtering a plant's own hydraulic, quench, EDM, and gear oils. | View → |
Technical, operating, maintenance, and EHS requirements
Evaluate system sizing, operating requirements, maintenance support, projected savings, and waste reduction for the facility.
- Sizing · specs · compatibility
Plant Engineer
Get GPM sizing, micron ratings, and compatibility for your exact coolant, confirmed by an engineer who reviews your fluid and application.
Select coolant equipment → - Sump cleaning · media · upkeep
Maintenance Manager
Review sump-cleaning time, filter media, routine ownership requirements, replacement parts, and technical support.
Review sump cleaning → - Payback · capital request
Operations / Plant Mgr
Estimate payback, potential reductions in new coolant purchases, disposal savings, and multi-plant standardization requirements.
Estimate savings → - Waste · exposure · facility records
EHS Lead
Review coolant-waste reduction, fluid-handling practices, workplace housekeeping, and available product documentation for facility records.
See sustainability → - Parts · media · reorders
Existing owner
Identify available replacement parts, media, and documentation by model or nameplate number for current and legacy equipment.
Parts and support →
Machine-shop coolant recycling and filtration
- 01
When does shop-wide coolant recycling make sense?
C.R.O.S.S. is evaluated when coolant is managed across multiple machines and consumption, contamination, disposal volume, or service workload calls for coordinated recovery. Machine count alone does not determine fit. Operations focused on individual reservoirs may be better served by T.O.S.S. for tramp-oil control or the Green Machine for sump cleaning.
- 02
How is a C.R.O.S.S. configuration selected?
An EdjeTech engineer selects model capacity and portable, piped, or hybrid coolant transfer from coolant volume, required processing rate, contaminant load, service schedule, and facility layout.
Review C.R.O.S.S. → - 03
Can I add recycling without trenching the shop floor?
Yes. A Green Machine or another portable device collects dirty coolant from individual reservoirs and delivers it to C.R.O.S.S. Clean coolant can be returned by portable equipment without central piping.
Batch configuration → - 04
Will recycling work with our specific coolant?
EdjeTech reviews the coolant, contaminant load, metals processed, and operating conditions before recommending equipment. Lead-contaminated and graphite-loaded coolant require application-specific evaluation.
Talk to an engineer → - 05
Do you still support equipment we bought years ago?
EdjeTech can identify available parts, media, documentation, and technical support for current and legacy equipment from the model or nameplate number. Availability depends on the installed model and component.
Parts & reorder →
Spend more time making parts
Reduce coolant waste and time spent on oil buildup and cleanouts, so your crew can focus on machining.
- Equipment guidance
Talk to an engineer
Reduce coolant work without disrupting your shop’s machining routine.
Talk to an engineer → - Product specifications
C.R.O.S.S.
Review machine-shop recycling models, performance, configurations, and options.
View C.R.O.S.S. → - Savings and payback
Savings calculator
Estimate potential coolant savings, disposal savings, and payback.
Estimate potential savings →