Guide · Tramp oil control & removal
Tramp oil sources, effects, and removal methods.
Tramp oil is unwanted oil from machine lubricants and leaks that contaminates water-based coolant. It can collect on the surface or circulate as small droplets, contributing to odor and shorter coolant life. Surface skimmers collect floating tramp oil, while coalescing separators also remove dispersed and loosely emulsified oil from the coolant. The right combination depends on your coolant, sump access, and how quickly oil enters the reservoir.
Where tramp oil comes from
Machine lubricants serve a necessary purpose, but they become contaminants when they reach the coolant reservoir. Way lubricant can be carried into the sump during machining, while hydraulic, gearbox, and spindle oils can enter through leaks. Oil on incoming parts can add to the contamination.
Once in the sump, the oil does not always remain as a visible layer. Pumps and agitation can break it into droplets and carry it through the coolant. This is why the appearance of the surface alone does not tell you how much oil remains in circulation. The main forms are:
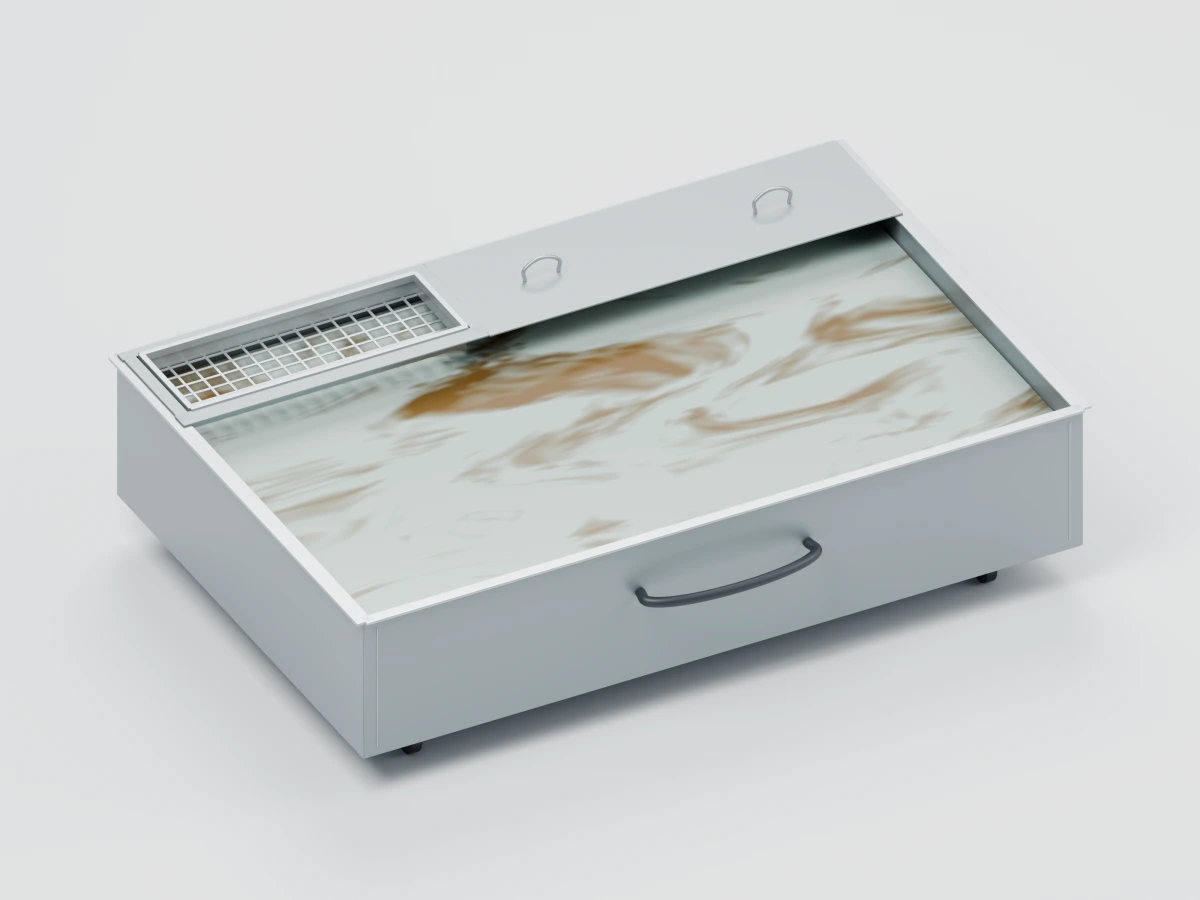
Free-floating oil
Free-floating tramp oil gathers in a layer or patches on the coolant surface. A surface skimmer can collect it where the pickup has access.
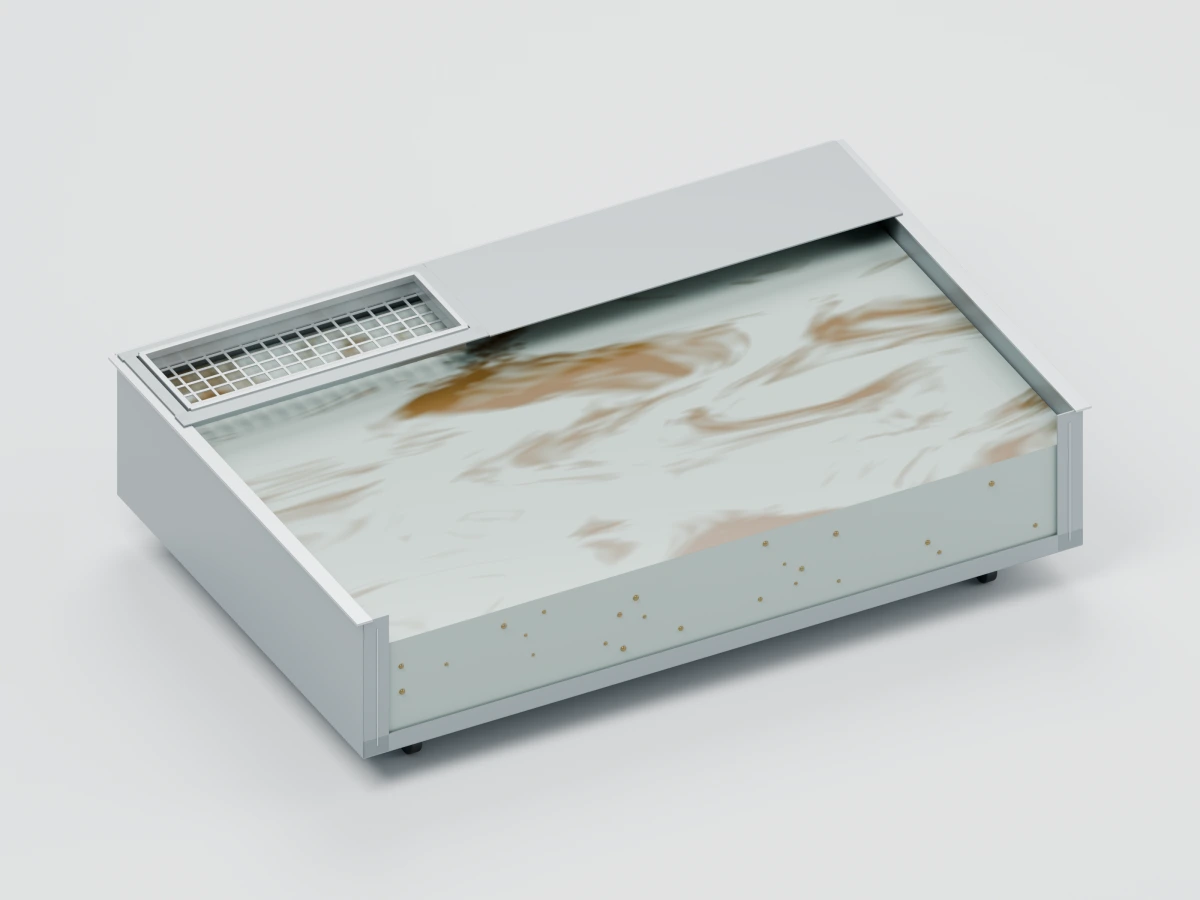
Mechanically dispersed oil
Mechanically dispersed tramp oil consists of small oil droplets mixed into coolant by agitation. These droplets can merge and rise when conditions allow, including within a coalescing separator.
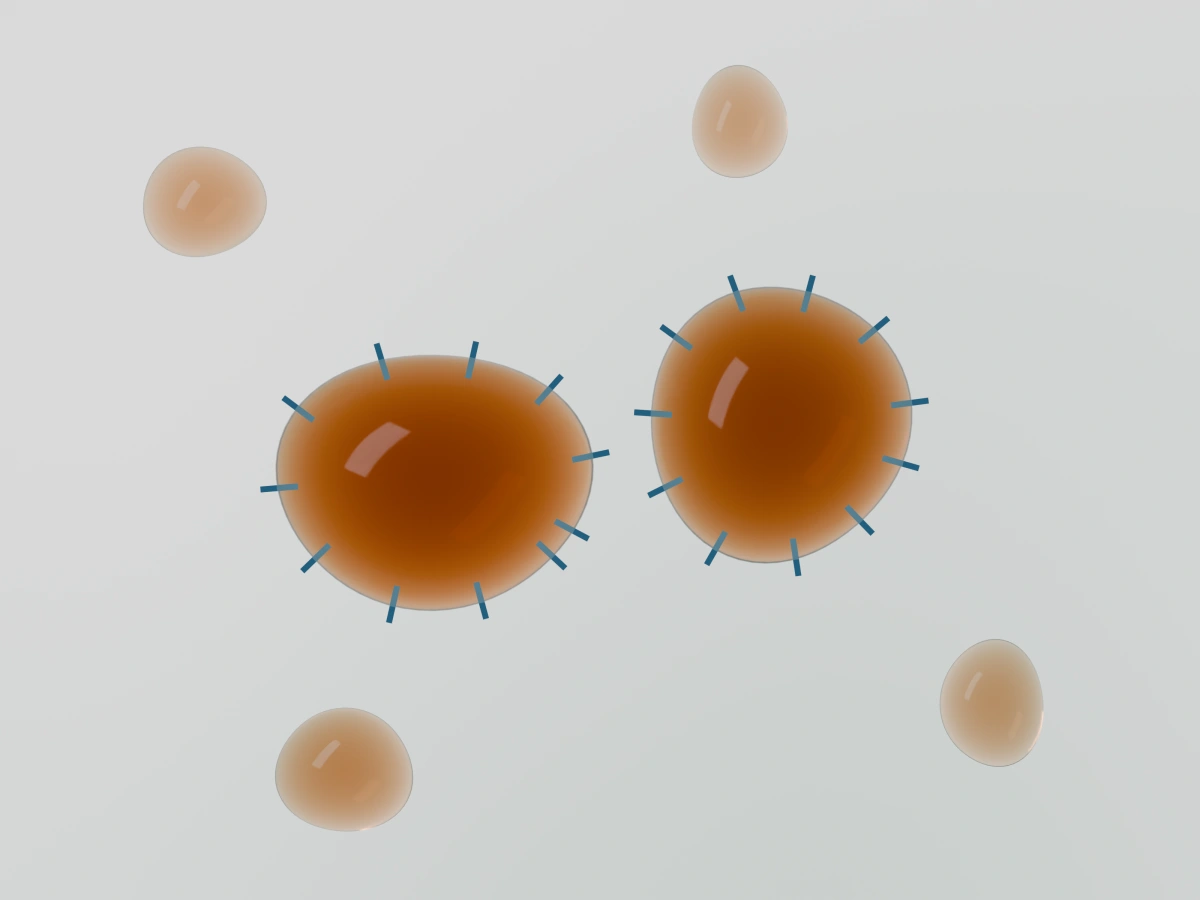 Tramp oil dropletsEmulsifiers may keep
droplets apart
Emulsified oil
Stable emulsions resist conventional gravity coalescing. Loosely emulsified tramp-oil droplets can merge into larger drops that rise to the coolant surface.
Free-floating, mechanically dispersed, and emulsified tramp oil can coexist in the same coolant reservoir. They also need to be distinguished from the oil intentionally included in a soluble-oil coolant formulation. Tramp-oil removal should take out foreign contamination while preserving the working coolant.
How tramp oil contributes to coolant odor
A persistent oil film changes more than the appearance of the coolant. In stagnant areas, it can contribute to a sequence of conditions associated with odor and degradation:
A surface film forms
Tramp oil gathers and spreads across the coolant surface.
Air contact decreases
The film can reduce oxygen transfer, particularly in stagnant fluid.
Bacterial growth is supported
Low-oxygen conditions can support bacterial activity in the coolant.
Odor and pH changes
Bacterial activity can produce odors and acids that degrade the fluid.
The consequences extend beyond smell:
Where the coolant is still suitable for reuse, separating the tramp oil can help extend its service life. The next step is to match the removal method to the form of oil present and the way it collects in the sump.
How to remove oil from coolants
Choosing a tramp-oil removal method starts with the form of oil present: free-floating, mechanically dispersed, loosely emulsified, or chemically emulsified. Oil that reaches the surface can be skimmed off. Droplets carried within the coolant need a separation stage suited to their behavior. Surface skimmers, coalescers, and centrifuges address these needs in different ways.
| Method | What it does | Where it fits / what to check |
|---|---|---|
| Surface skimmingBelt, disc, tube, or surface pickup | Collects free-floating oil that reaches the sump surface. Belt, disc, and tube skimmers lift oil onto a moving surface; suction and floating-weir pickups draw an oil-rich fluid stream. | Start here when oil gathers at an accessible surface. The pickup must reach that oil as the coolant level changes; turbulence can keep it away. Allow access to clean the pickup and scrapers, and check how much coolant leaves with the oil. A surface pickup alone does not separate dispersed droplets. |
| Coalescing separationSurface pickup + separator | A pump feeds collected coolant through media that brings small, physically separable oil droplets together. Larger drops rise and leave through a separate oil outlet; clarified coolant returns to the sump. | For ongoing removal of free, mechanically dispersed, and loosely emulsified oil. The oil must separate from the working coolant, with enough time in the separator for droplets to rise. Match process flow to the separator and oil loading. Solids prefiltration and access for media cleaning help maintain separation. |
| Centrifugal separationHigh-speed rotating separator | Uses centrifugal force to accelerate separation of fluids with different densities. Depending on the design, the equipment can also separate solids. | Consider for combined oil and fine-solids removal with a centrifuge designed for liquid-liquid separation. A solids-only centrifuge serves a different job. Confirm that treatment preserves the coolant formulation. Compare the required utilities and process flow, and how collected solids are removed, including manual bowl cleaning where applicable. |
Compare like-for-like ratings. A separator's rating in gallons per minute (GPM) describes the coolant stream it processes, not gallons of tramp oil recovered. Oil loading and separation conditions also determine the equipment size.
The distinction between collection and separation is important. A belt or disc skimmer lifts oil from the surface. A suction or floating-weir pickup collects an oil-rich stream that can then be sent through a coalescer. Top suction and coalescing therefore describe different stages of the same process, rather than competing removal methods.
The oil-skimmer guide for machine shops explains the pickup designs in more detail, including how access, liquid-level changes, and turbulence affect selection.
In a sump-side installation, the separator draws from where the oil collects and returns the treated coolant to the same reservoir. Recovered oil follows a separate line to a collection container:

- 1Oil-rich fluid to separator
- 2Treated coolant to sump
- 3Recovered oil to container
How oil coalescers work
Inside a coalescer, small oil droplets contact media that helps them meet and merge. As the drops become larger, they rise more readily through the fluid and collect in a layer that can be removed separately. The cutaway shows how this separation stage fits alongside bag filtration in a T.O.S.S. T1:
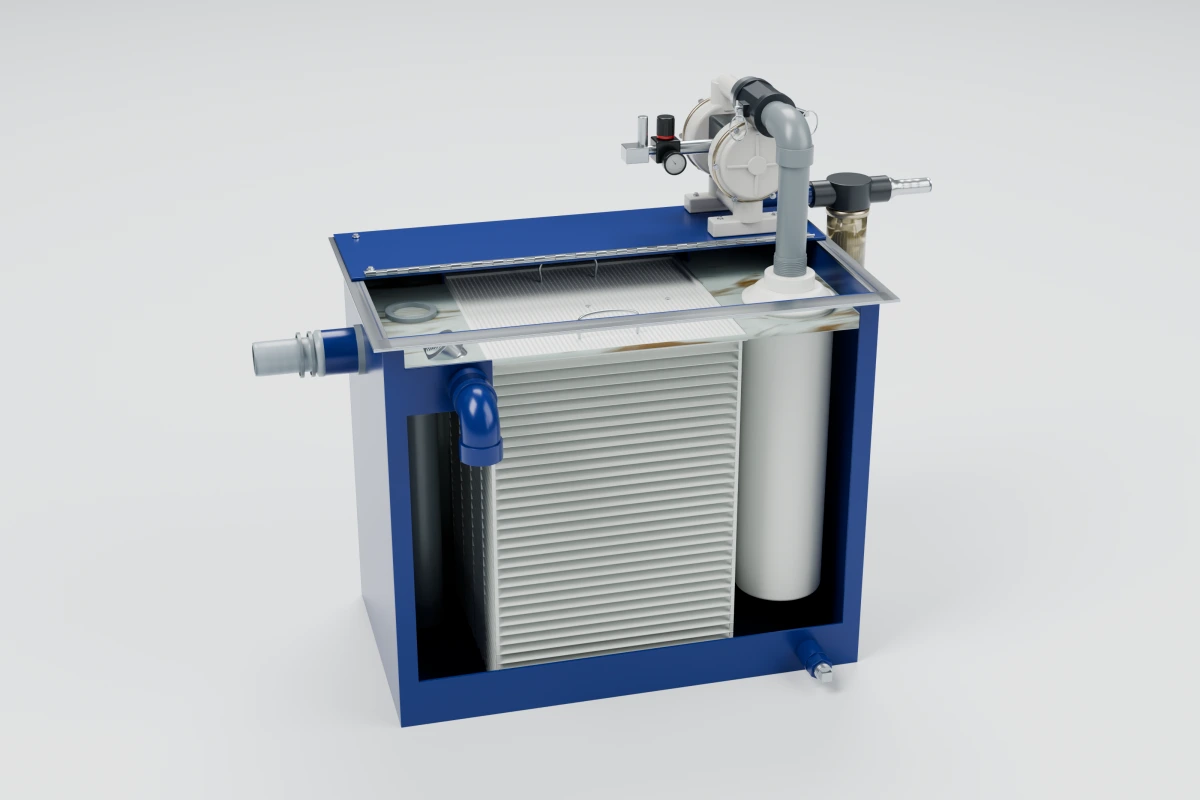
- AOil-rich coolant inlet
- BBag filter
- CCoalescing media
- DRecovered oil outlet
- ECoolant return
In T.O.S.S. equipment, coalescing is part of a continuous collection, filtration, and return process:
Collect and filter the fluid
The floating pickup draws surface oil and coolant from beneath the surface, carrying dispersed oil and suspended solids into the separator. Bag filtration removes solids before the fluid reaches the coalescing media.
Combine the oil droplets
As coolant passes through the polypropylene media, oil droplets contact the surfaces and merge into larger drops.
Separate the oil by gravity
The larger drops release from the media and rise into a floating layer in the separation chamber. This oil layer is a normal part of separation: it collects recovered oil for discharge while coolant continues flowing beneath it.
Recover oil and return coolant
Separated oil drains to collection, while clarified coolant crosses the outlet weir and returns to the reservoir.
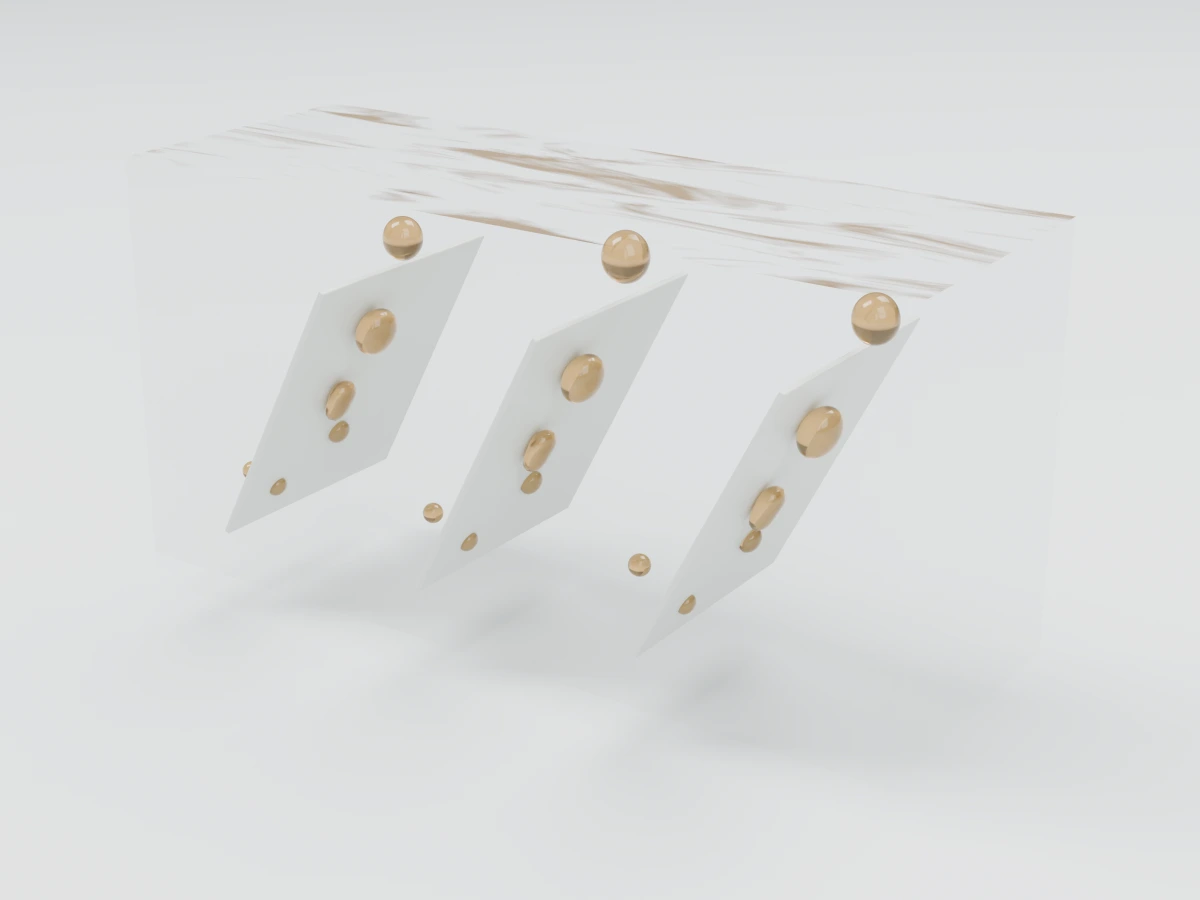
- 1Small oil droplets
- 2Drops combine on media
- 3Larger drops rise
Why droplets need to combine
Coalescing depends on oil droplets combining into larger drops that can separate from the coolant. T.O.S.S. uses coalescing to remove free-floating, mechanically dispersed, and loosely emulsified tramp oil. A stable chemical emulsion resists that process, so unclear separation behavior calls for a review of the fluid chemistry. The fluid-compatibility guide describes a simple separation check that can help inform that review.
Flow, pump selection, and the condition of the media also affect the separation process. These are covered in the full guide to how tramp-oil coalescers work. Once the method is suitable for the fluid, the next decision is how the equipment will serve the operation.
One sump, a larger reservoir, or the whole shop?
Coalescing tramp-oil separators are available as portable units or equipment dedicated to a particular reservoir. The choice depends on how quickly oil enters the coolant, the volume being treated, available utilities, and whether one machine or several need attention.
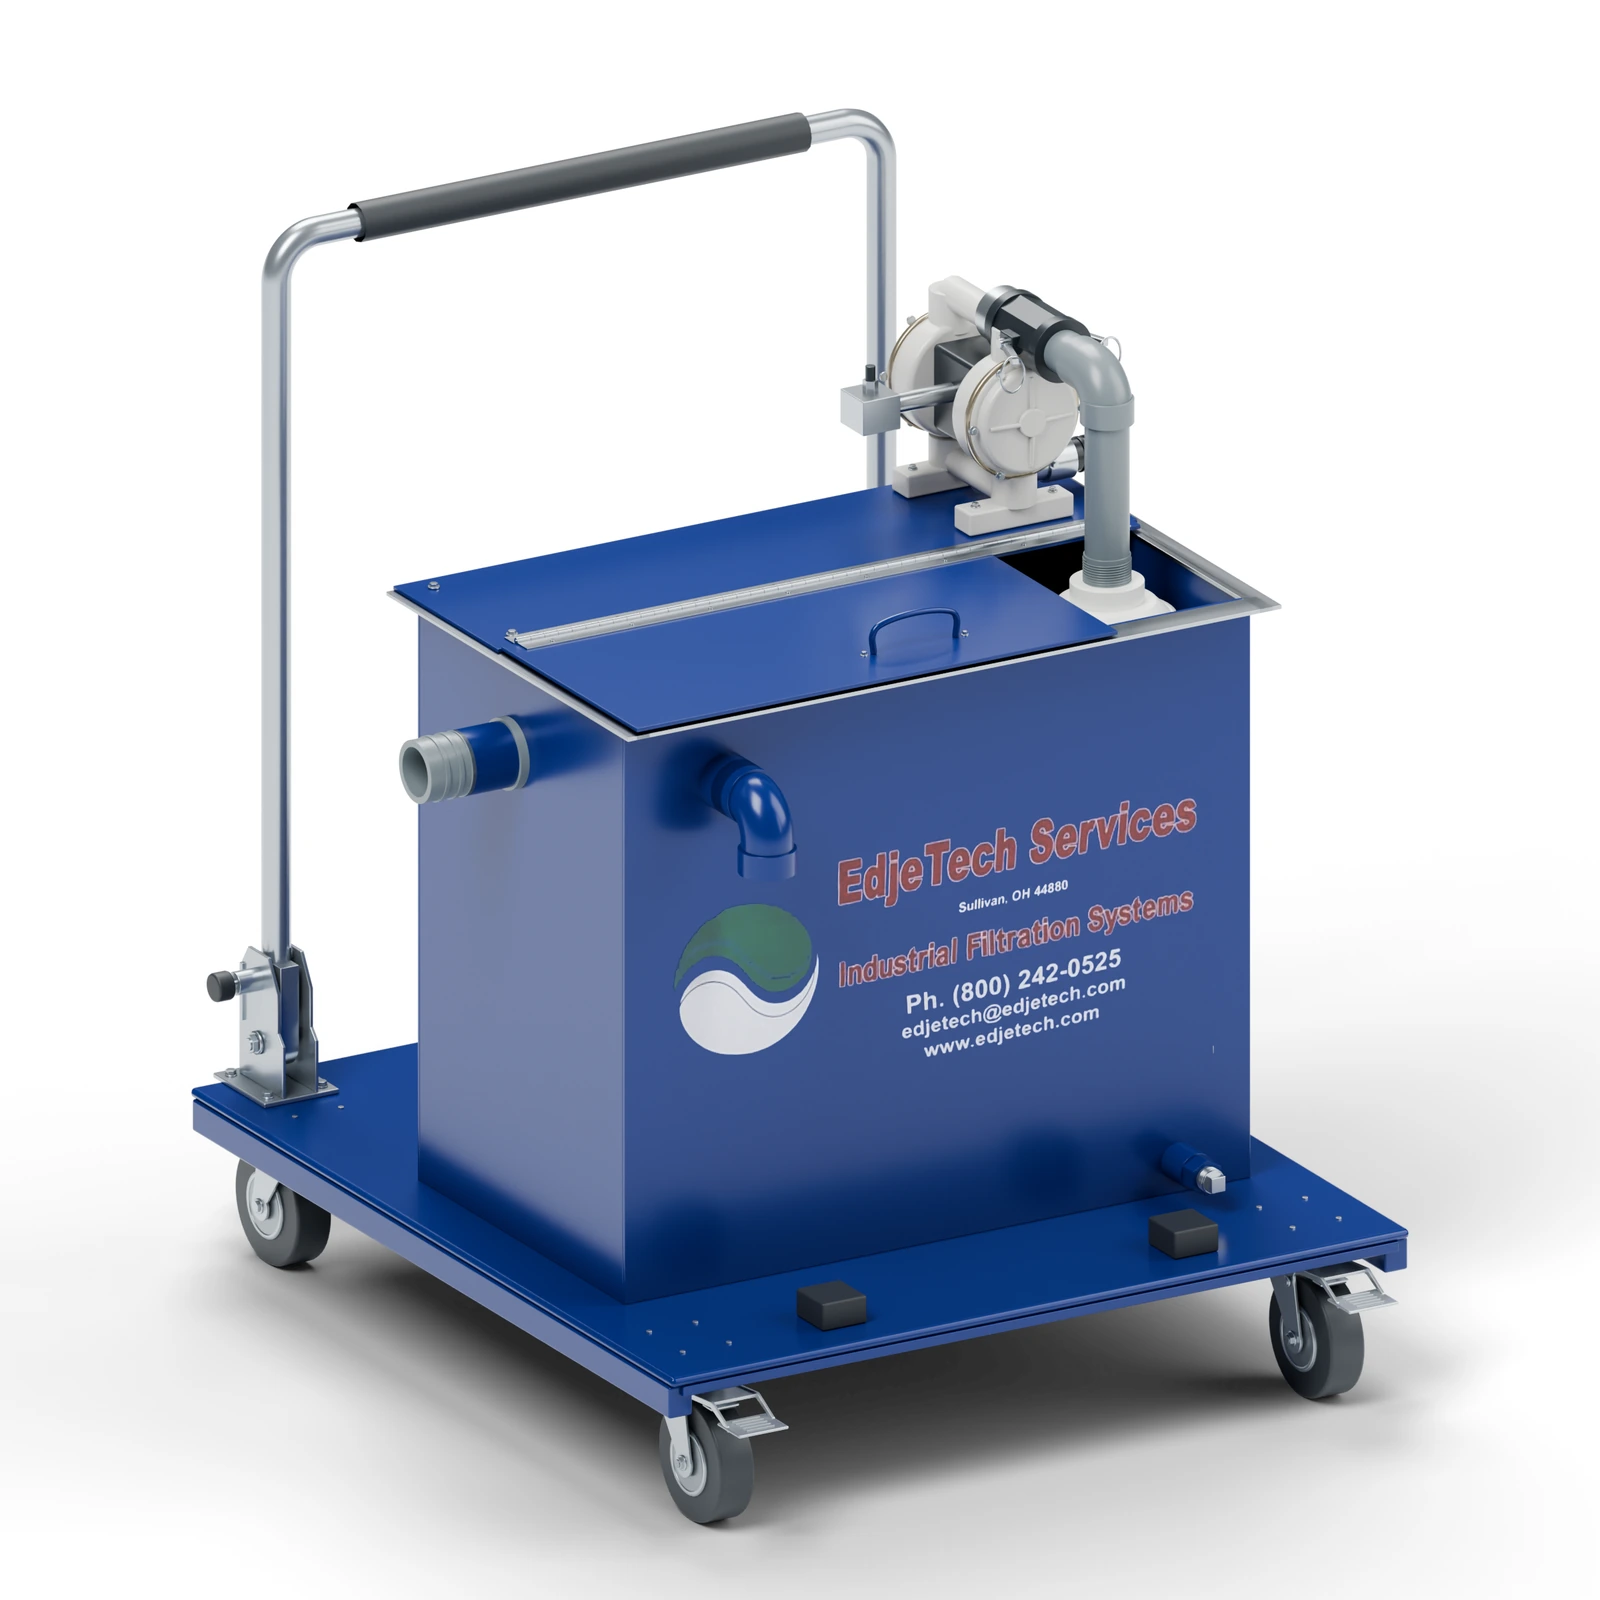
Portable treatment with T.O.S.S. T1
A portable separator is useful when equipment needs to move between individual sumps. The T.O.S.S. T1 treats one reservoir at a time at 2 GPM using shop air, combining surface pickup, solids filtration, and coalescing in a compact unit.
View T.O.S.S. T1 specificationsFor temporary use, EdjeTech also offers T1 rental and lease options.
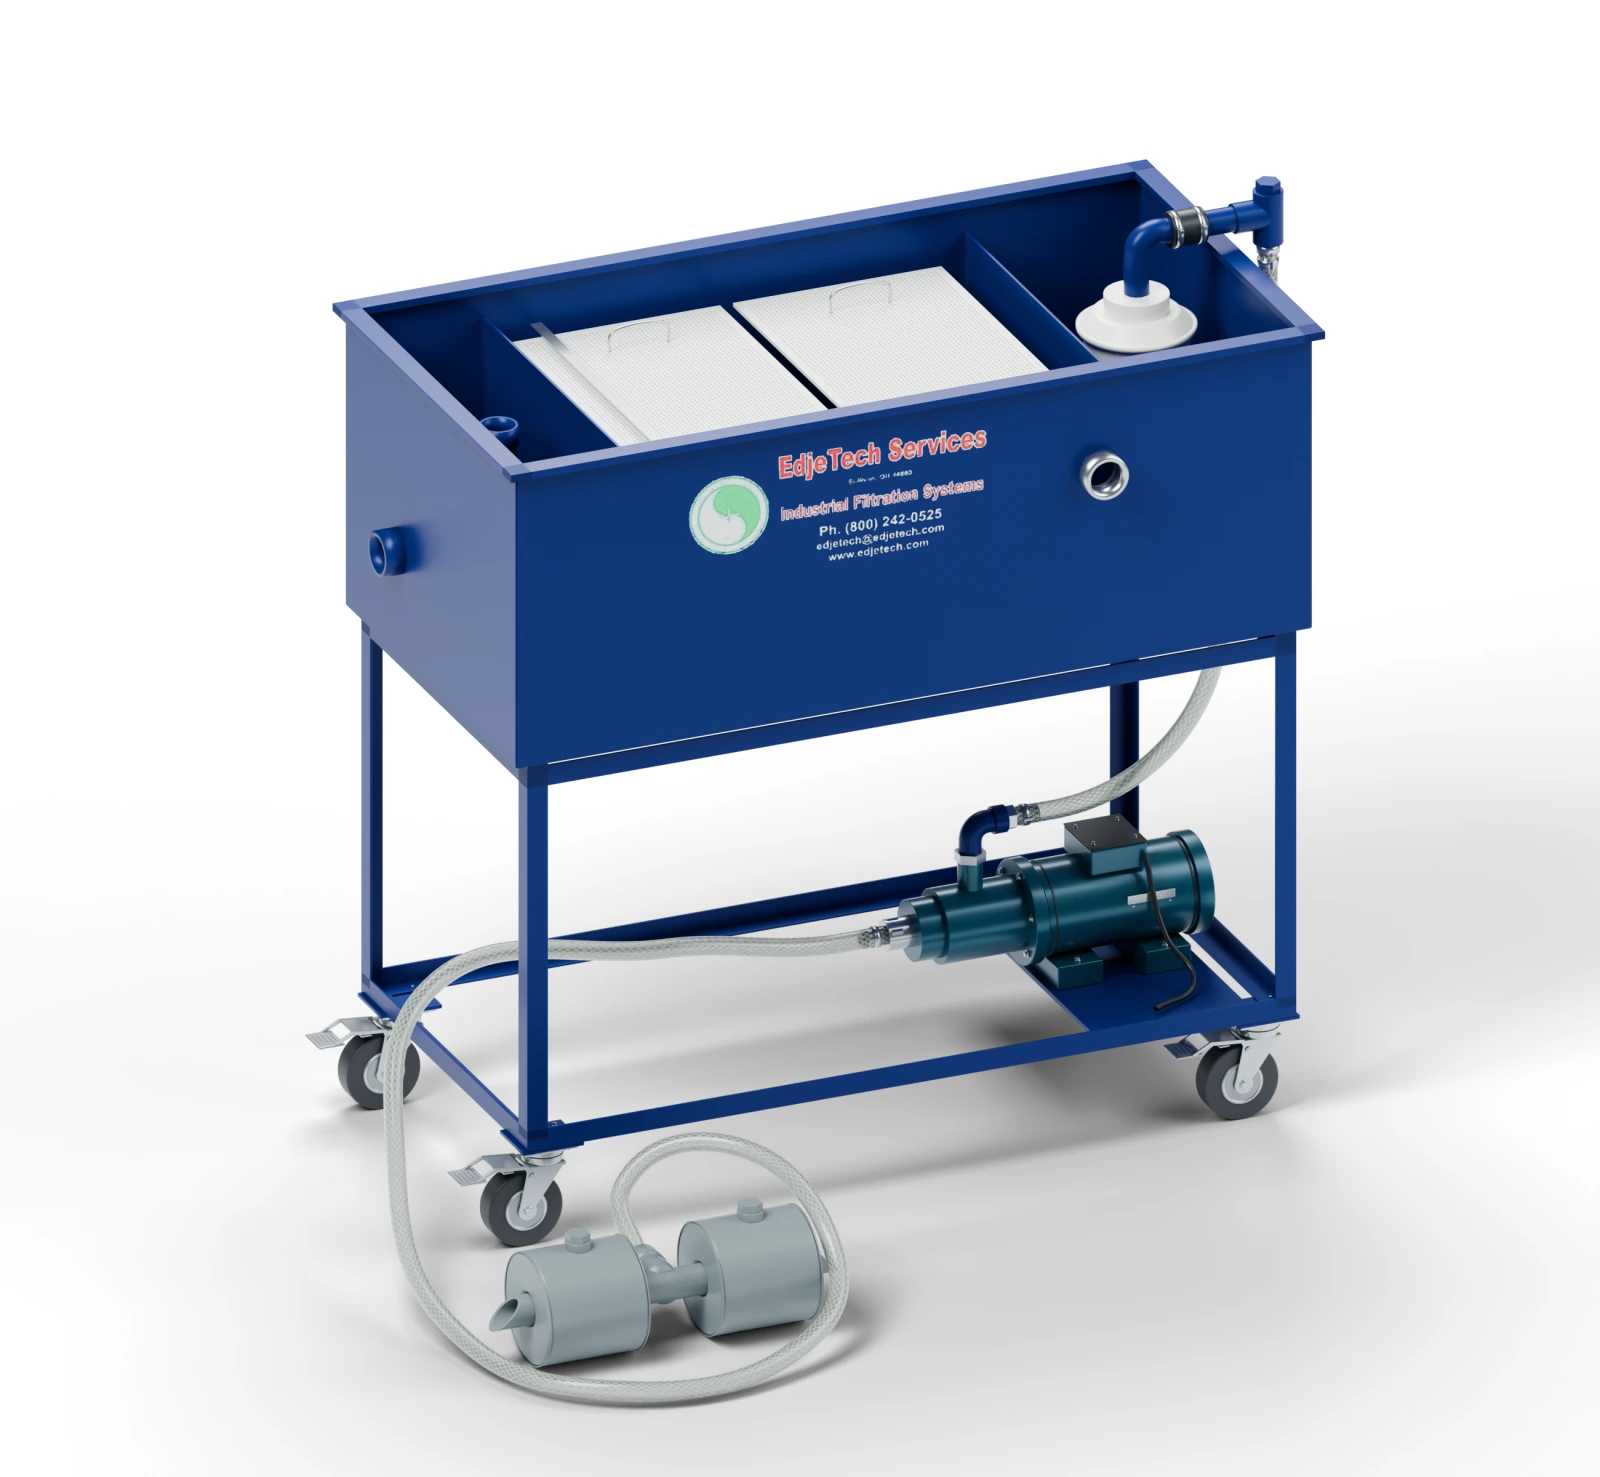
Dedicated treatment with the T.O.S.S. series
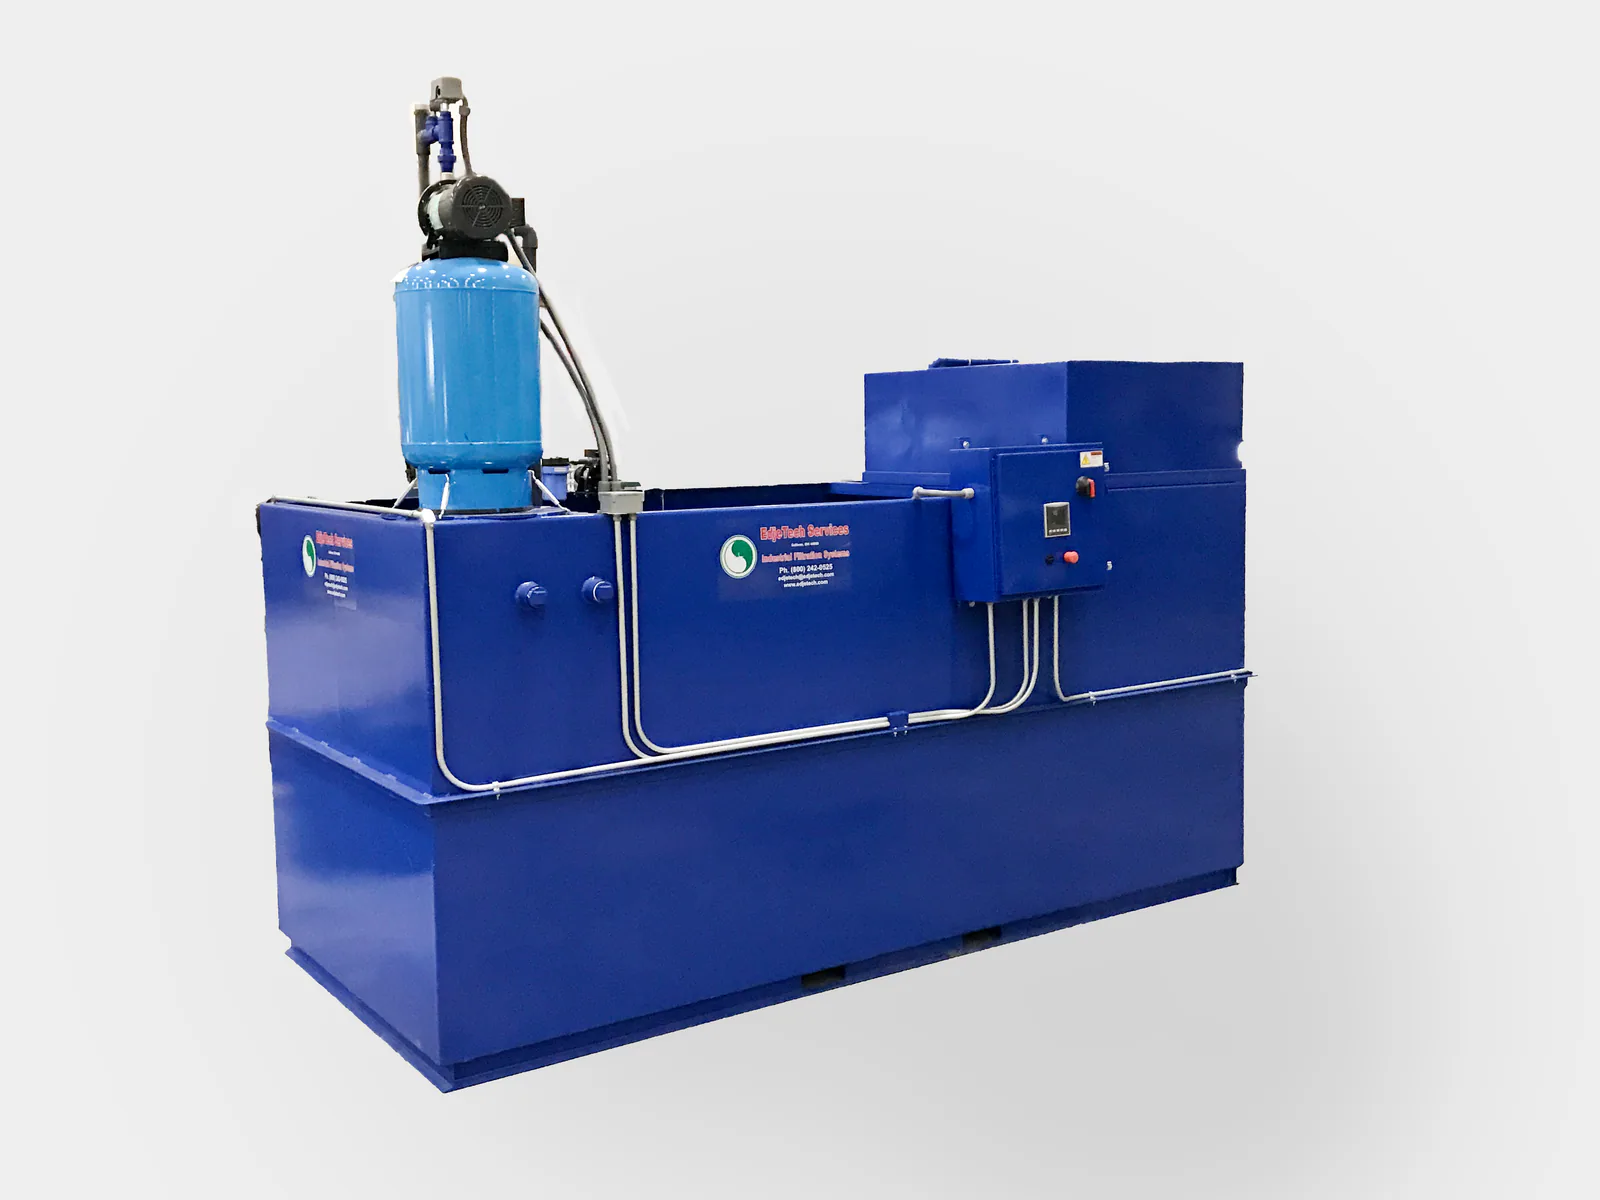
When oil loading calls for ongoing treatment at a particular sump, reservoir, coolant pit, or parts washer, a dedicated separator can stay with that location. The T.O.S.S. series offers seven standard sizes rated from 2 to 50 GPM, with pickup and pump options to match the application. Custom sizes are also available.
Compare T.O.S.S. modelsCompare all T1 and standard T.O.S.S. models
Shop-wide coolant recycling with C.R.O.S.S.
For shops managing tramp oil, suspended solids, and coolant concentration across several machines, C.R.O.S.S. combines tramp-oil removal, particulate filtration, coolant replenishment, and clean-fluid storage. Dirty coolant is brought to the station; an optional Coolant Return System distributes clean coolant through facility piping.
See how C.R.O.S.S. central recycling worksKeep tramp oil from building up again
Ongoing tramp-oil control requires attention to both lubricant entry and oil removal. Compare where tramp oil collects and how quickly it reappears after removal under similar operating conditions. These observations help identify whether to investigate lubricant entry, pickup access, or separator maintenance.
- Oil returns quickly after removal
- Trace hydraulic, gearbox, and spindle leaks with the maintenance team. Check way-lubrication delivery against the machine manufacturer's requirements; do not reduce necessary lubrication to limit oil in the sump.
- Oil gathers away from the pickup
- Check whether baffles, changing fluid levels, or return-flow turbulence prevent oil from reaching it. Pickup location and access matter as much as the amount of oil visible elsewhere in the tank.
- Oil remains, but collection slows
- Check the pickup, hoses, filter condition, and coalescing media using the equipment's maintenance instructions. A drop in collected oil may reflect reduced flow or dirty media rather than less contamination.
A clearer surface does not establish the overall condition of the coolant. For concentration, pH, other contaminants, and fluid-life decisions, use the CNC coolant-management guide. Keeping tramp oil under control is one part of that wider program.
Common questions about tramp-oil removal
Can T.O.S.S. operate while the CNC machine is running?
Will removing tramp oil restore coolant that smells rancid?
Can one separator serve several machines?
What happens to recovered tramp oil?
Keep recurring tramp oil under control
Remove unwanted oil so your coolant can stay in service and keep doing its job at the machine.
Building the business case? Estimate coolant savings and payback